STAGE 01
Formulation & Feasibility
Excipient compatibility screening, flowability profiling, and botanical active stabilization.
Gate: Pre-formulation Report
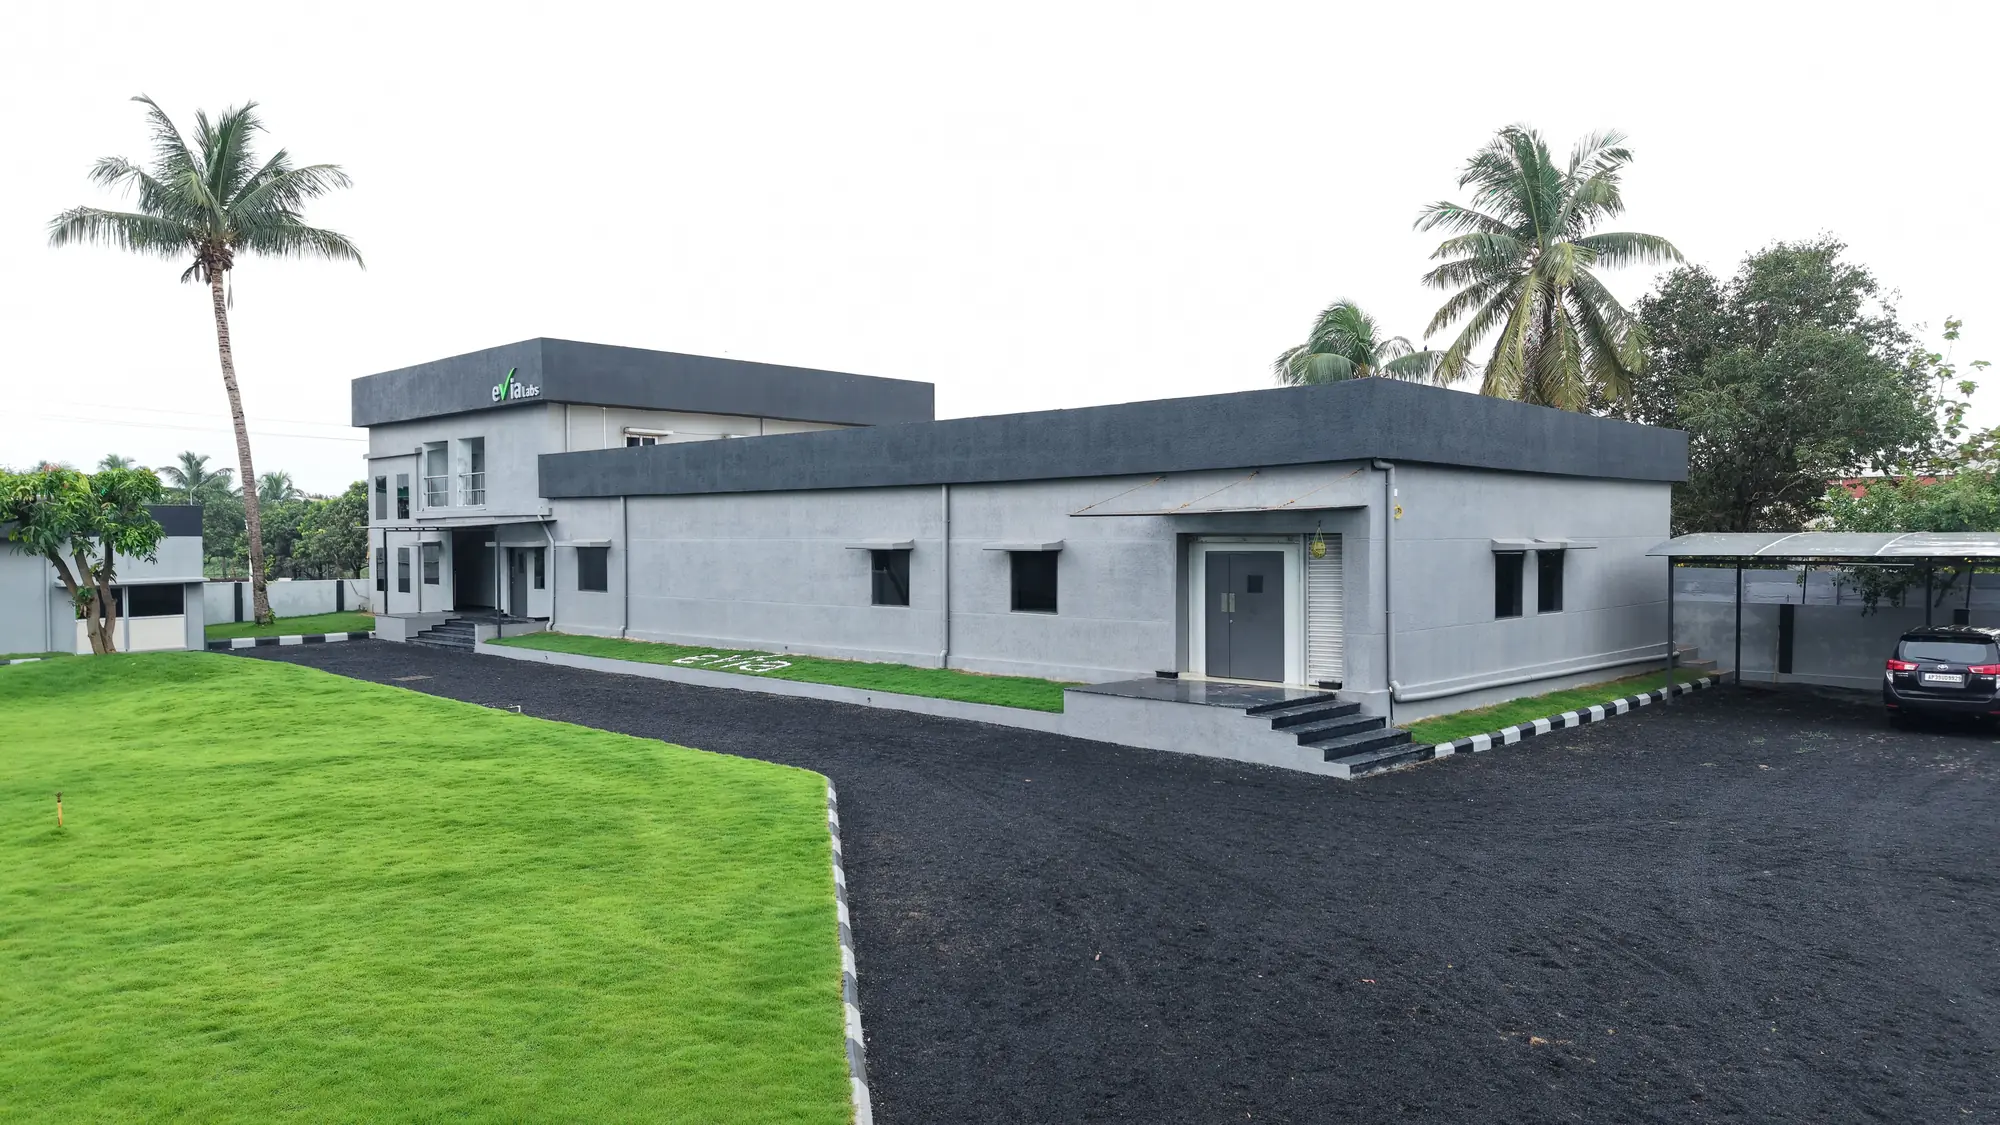
Operating state-of-the-art modular Class 100,000 / engineered under stringent WHO-GMP guidelines. eVia Labs converges advanced cGMP standard operating procedures with pharmaceutical-grade solid oral dose and encapsulation.
Confidential technical dossiers & protocol consultations upon NDA
From molecule sourcing through commercial batch dispatch, every milestone requires formal analytical clearance and quality oversight before stage progression.
Excipient compatibility screening, flowability profiling, and botanical active stabilization.
Gate: Pre-formulation Report
Small-scale pilot batches, hardness curves, disintegration runs, and client sign-off.
Gate: Pilot CoA & Client Approval
Regulatory filing support and FSSAI product category endorsement.
Gate: Regulatory Clearance Dossier
Full scale blending, compression, or encapsulation under monitored cleanroom HVAC specifications.
Gate: Batch Manufacturing Record
Complete microbiological testing, heavy metals screening, assay checks, and QA document sign-off.
Gate: Final Release Certificate
Hermetic sealing, tamper-evident outer boxing and ambient staging.
Gate: Commercial Dispatch Waybill
“Many manufacturers can make a product once. Few can repeat it with identical purity, dissolution timing, and assay records across every single cycle.”
Our quality verification protocol operates autonomously from commercial manufacturing schedules. Analytical release requires uncompromised quantitative passes at all three verification checkpoints.
100% of botanical extracts, active vitamins, and functional minerals undergo spectroscopic identity verification, moisture analysis, bulk density validation, and assay qualification before automated release into active inventory.
Continuous sampling every 30 minutes during active production runs. Tablet thickness, hardness profiling, friability (<0.8%), disintegration time checks, and capsule fill weight dispersion indexing ensure batch uniformity.
Comprehensive Certificate of Analysis (CoA) generation including active potency retention, stability assay, dissolution curves, microbial absence (E. coli, Salmonella, S. aureus), and leak integrity testing for blisters.
Our manufacturing facility is independently certified for the manufacture of food and health supplements and nutraceuticals.
Good Manufacturing Practice
Issued by MQA Certification
Quality Management System
Issued by United Accreditation
Certificate of Compliance
Issued by UKAF Cert
Certificate of Compliance
Issued by MQA Certification
Review our cleanroom parameters, HVAC protocols, and analytical chromatography specifications. We provide complete technical batch dossiers and consultation sessions upon NDA.